


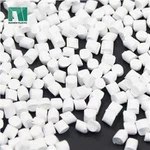

High-End PP PE Color Masterbatch for Blown Film and Plastic Products
Our company pays attention to improve the profitability and cash creation ability of its Drip Irrigation Black Masterbatch, PE carrier black masterbatches, Recycled Plastic Defoaming Masterbatch in production and operation. We will continue to use diversified thinking and talents to deal with opportunities and challenges, and continue to provide consumers with services in a meaningful way. Our company realizes the diversification and serialization of products, which can meet the needs of various customers all around the world. We believe that any outstanding technology, product and service can only be recognized by customers and create value for customers if the quality is excellent. Our company attaches great importance to product quality and regards quality as life.
Hygienic/food grade color masterbatch adopts high qualified imported pigments, virgin polyethylene resin and imported dispersing agents. All the raw materials for masterbatch come with Hygienic or food inspection reports, such as SGS, ROHS, REACH, FDA.
Index | Value |
Carrier | PE/PP/EVA |
Pigment | Rutile Titanium Dioxide |
Titanium Dioxide Content | 20% - 70% |
MFI (21.6KG/190°C) | 10-30g/10min |
Intermiscibility | PE/PP |
APPLICATION:
Suitable for milk films, lunch boxes, drinking water pipes, sanitary napkins, diapers, cast films, food packaging films, etc.

Packing & Shipping:

Our company carefully manufactures high-quality High-End PP PE Color Masterbatch for Blown Film and Plastic Products that are well received at home and abroad. We ensure excellence in production management and lean production methods. We must gradually standardize the company's various business management activities in accordance with the modern enterprise management system, so that the responsibilities and rights of the company's various departments and employees can be balanced with each other.
You Might Also Like




Send Inquiry